

Table of Contents
1. Introduction to Heat Sealers for Food Packaging
1.1 What is a Heat Sealer?
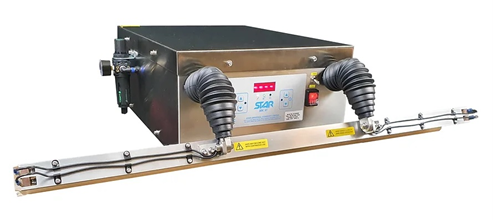
A heat sealer for food packaging is a critical piece of equipment used to create airtight, tamper-evident packaging by bonding materials like plastics or foils through heat and pressure. This process ensures freshness, safety, and quality in food products. Heat sealing machines work by clamping heated sealing elements around the packaging material, melting and bonding the materials together to form a hermetic seal.
1.2 Importance of Heat Sealing in Food Preservation
Heat sealing plays a pivotal role in extending product freshness, maintaining nutritional value, and reducing food waste. By preventing the entry of oxygen and microorganisms, heat sealing protects the product from degradation and contamination. It also enhances visual appeal and preserves sensory qualities such as colour, texture, and taste. Learn more about heat sealing technology and its role in food safety.
2. Types of Heat Sealers Available
2.1 Handheld Heat Sealers
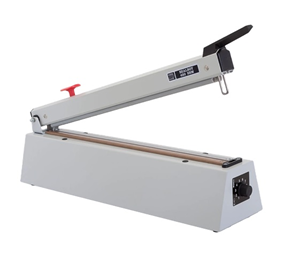
Handheld heat sealers are compact, user-friendly tools designed for small-scale or mobile food packaging operations. Ideal for businesses with lower output needs, these devices offer flexibility and ease of use.
Explore compact heat sealers for industrial use – make your food storage effortless!
2.2 Automatic Heat Sealers
Automatic heat sealers are suited for high-volume commercial food packaging. These machines automate the sealing process, offering consistent performance and reducing manual labour, making them perfect for busy production lines.
Upgrade to automatic heat sealers for food packaging – perfect for busy industrials!
3. Choosing the Right Heat Sealer
3.1 Factors to Consider
When selecting heat sealers for food packaging, consider:
- Material compatibility (e.g. LDPE, laminates)
- Packaging format (e.g. pouches, trays, clamshells)
- Production volume and speed
- Precision requirements (temperature, pressure, dwell time)
- Energy efficiency
- Maintenance and downtime risk
Obeeco can help evaluate your needs and identify the best sealing technology for your operation. Contact us for a consultation.
3.2 Comparing Models and Brands
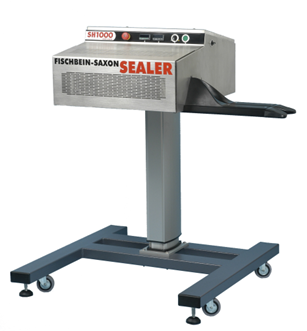
Obeeco offers various sealing solutions including benchtop sealers for smaller-scale applications and in-line machines for industrial throughput. We guide clients in matching sealing equipment to their operational needs, ensuring reliability and compliance.
4. Benefits of Using Heat Sealers in Food Packaging
4.1 Enhanced Shelf Life
Heat sealing creates an airtight, hermetic seal that prevents oxidation, moisture ingress and microbial contamination. This extends product shelf life, reduces spoilage and improves shelf performance.
Invest in reliable heat sealers for food preservation – order yours now!
4.2 Reduced Waste and Cost Efficiency
Heat sealing produces robust, tamper-evident packaging that reduces damage during handling. Resealable options also reduce food waste. Efficient packaging means fewer resources used and less environmental impact.
Sealing also maintains the nutritional value of food by reducing exposure to oxygen and external contaminants.
5. Compliance and Regulations in Ireland and Northern Ireland
5.1 Food Safety Standards
In Ireland and Northern Ireland, heat sealing must align with FSAI and FSA standards. Proper sealing protects against contamination and ensures food remains safe throughout its lifecycle.
5.2 Packaging Regulations
Packaging must comply with European and UK legislation concerning recyclability, waste reduction and food contact safety. Obeeco’s heat sealing equipment supports compliance through precision sealing and durable packaging formats.
6. Conclusion
6.1 Future Trends in Heat Sealing Technology
Emerging developments in heat sealers for food packaging include:
- Lower energy consumption models
- Smart sensor integration
- Compact modular systems
- Eco-friendly sealing material compatibility
As energy costs continue to rise, manufacturers are seeking more sustainable and cost-effective machinery. Newer heat sealer models are being developed with improved thermal insulation and energy management systems to significantly reduce power usage without sacrificing sealing quality.
Smart sensors and automation are becoming increasingly popular, allowing for real-time diagnostics and adaptive sealing based on material feedback. These features improve sealing consistency, reduce operator error, and enhance product quality.
Compact modular designs are also gaining traction, particularly for businesses with space constraints or those looking for scalable solutions. These systems can often be upgraded as production volumes grow.
Lastly, compatibility with compostable and recyclable materials is a key focus area. As the demand for sustainable packaging rises, heat sealers must adapt to new substrates without compromising seal integrity.
The flexibility of heat sealing ensures its continued importance across all sectors of the food industry.
6.2 Resources for Further Information
Visit our dedicated heat sealing solutions page or explore other food packaging systems for additional integration options.
FAQs
1. How do I choose the right heat sealing machine for my business?
We offer a free consultation to help assess your production needs, materials, and budget. Contact us and our team will guide you in selecting the most suitable model.
2. Do you offer installation services for heat sealing equipment?
Yes, we provide full installation and setup support after purchase. Our technical team ensures that your equipment is installed correctly and ready for operation.
3. What support do you offer after the sale?
We provide technical guidance, maintenance tips, and operational support to ensure your equipment runs smoothly. For service inquiries, contact us.